High-efficiency industrial ventilation, automated spot cooling, cleanroom environmental management, and compressor waste heat recovery across bottling lines.
Waste Diversion
Water Savings
Energy Savings
Solar Offset
* Audited across bottling hall, syrup preparation zones, and warehousing facilities.
Reduced bottling hall ambient peak thermal stress by 6.5°C while trimming auxiliary fan electricity consumption by 38%.
High-efficiency industrial ventilation, automated spot cooling, cleanroom environmental management, and compressor waste heat recovery across bottling lines.
Harnessed compressor thermal rejection for boiler feedwater preheating, saving thermal fuel.
Targeted high-velocity displacement diffusers focusing conditioned air directly on operator stations.
Controlled pressure gradients preventing dust ingress into bottling and clean packaging areas.
Smart scheduling and temperature reset curves responsive to factory ambient loads.
Delivering heavy-duty industrial environmental control that drives high-throughput manufacturing productivity while hitting strict decarbonization targets.
 IGBC Platinum Certified
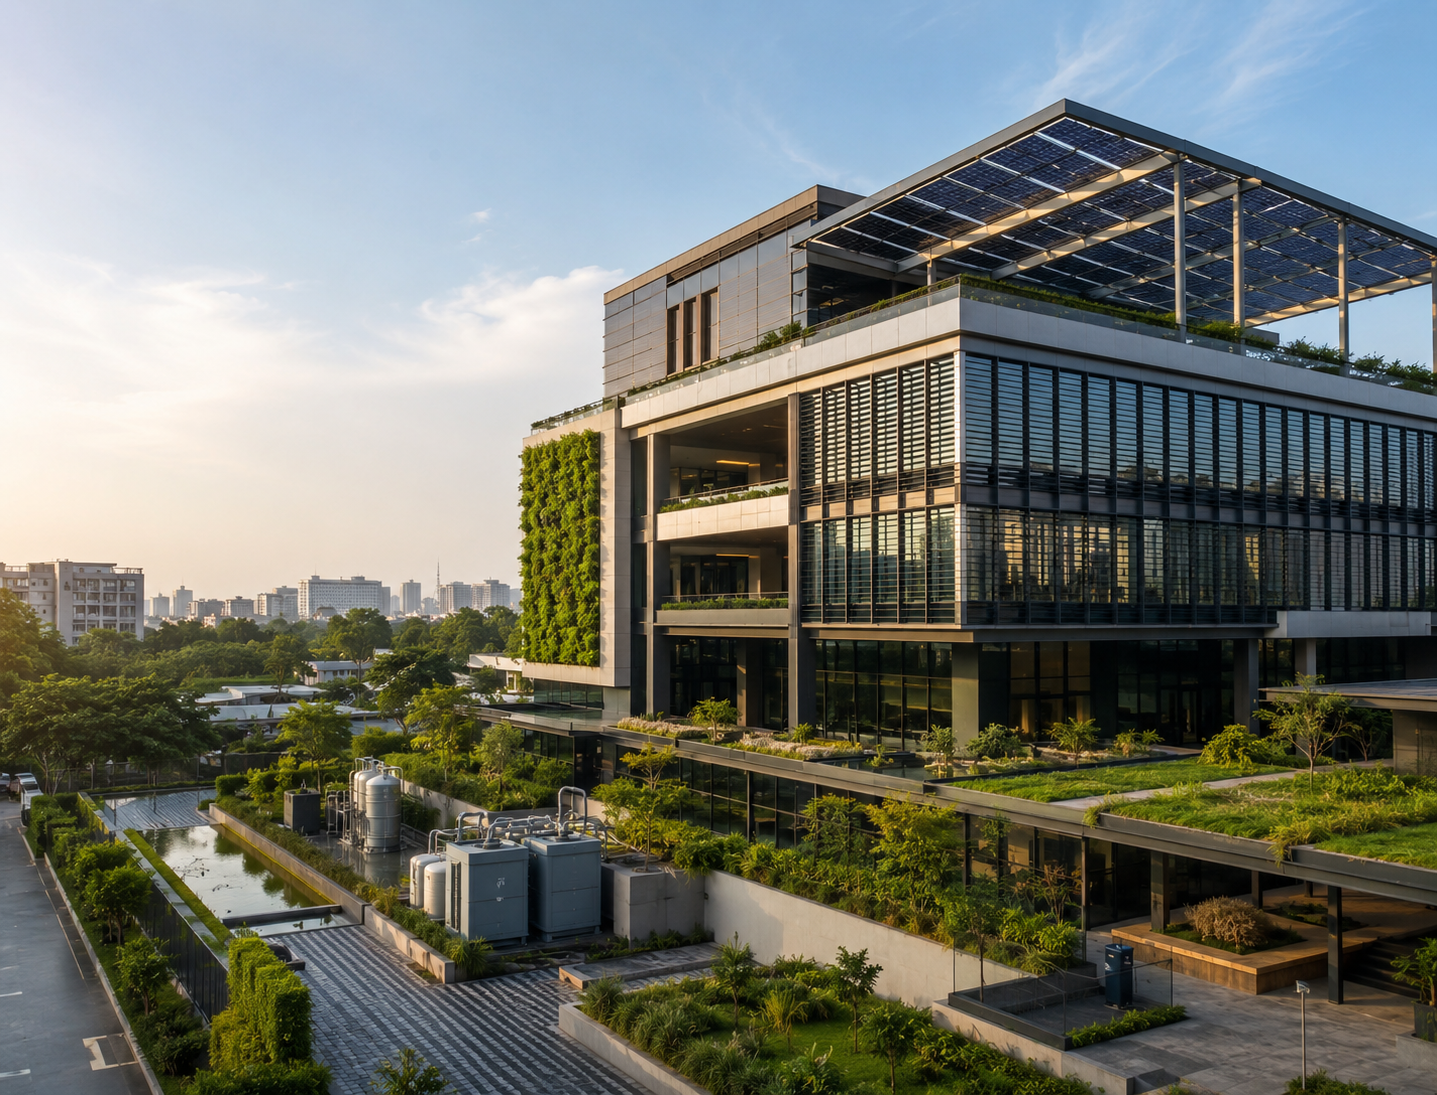 LEED Platinum Certified
 NABH & ISO Class 5 Compliant